Business Details
25 Years
experience
Emergency
services
Leading Manufacturer of Chemical Process Equipment
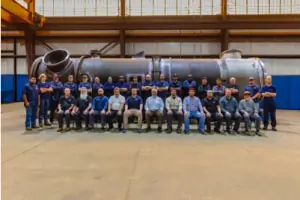
Apex Engineered Products, headquartered in Clark, Pennsylvania, specializes in the design and fabrication of premium chemical process equipment for major producers worldwide. Established in 2001, we focus on mitigating corrosion through advanced materials like titanium, zirconium, tantalum, and nickel alloys, offering innovative solutions since our inception. Our expertise extends to industries including chemical, petrochemical, chlor-alkali, steel processing, and more, with satellite manufacturing facilities in Tampa, Florida, and India. Our team of engineers, designers, and welders leverages state-of-the-art technology, including K-Tig welding stations and Omax water jets, to deliver precision-crafted equipment. We adhere to rigorous quality standards, including ASME Section VIII Div. 1 U Stamp and National Board R Stamp certifications, ensuring compliance with global requirements.Our 24/7 field services provide rapid on-site repairs, alterations, and upgrades, minimizing downtime for clients. Recognized by accreditations from The Chlorine Institute, ASME, and NACE International, we prioritize client satisfaction through transparent communication and cost-effective solutions. Our commitment to innovation is highlighted by pioneering technologies like the HXT Tube, which enhances heat exchanger efficiency by 30 - 50%. Trusted by leading chemical producers worldwide, we combine decades of experience with cutting-edge methodologies to build equipment synonymous with reliability and scalability. Our mission is to empower industries with corrosion-resistant solutions that withstand extreme environments while maintaining operational excellence.
Services
Heat Exchangers
Pressure Vessels
Field Services
Graphite Equipment
Nickel Alloy Fabrications
Details
- Year established: 2001
Highlights and features
- 24/7/365 on-site field services for rapid equipment repairs.
- Expertise in exotic materials like titanium, zirconium, and nickel alloys.
- Global manufacturing capabilities with facilities in the U.S. and India.
- ISO-certified quality assurance and compliance with ASME standards.
- Innovative HXT Tube technology improves heat exchanger efficiency by 3050%.
Associations and certifications
- The Chlorine Institute
- ASME
- National Board of Boiler and Pressure Vessel Inspectors
- AIChE
- NACE International
- ISNetworld
- TUV Nord
- TEMA
What people say
Delivered a top-notch product
Superior workmanship
Excellent team
Performing better than expectations
Responsive and timely
Services
Heat Exchangers
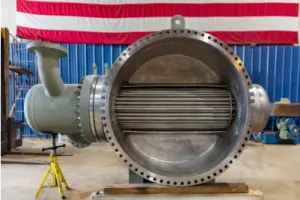
We design and fabricate high-performance heat exchangers using corrosion-resistant materials like titanium, zirconium, and nickel alloys. These systems ensure efficient thermal transfer in harsh chemical environments, serving industries such as chlor-alkali, petrochemical, and steel processing. Our solutions combine advanced engineering with materials science to deliver durability and reliability.
Field Services
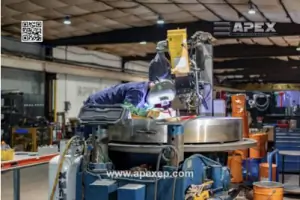
Our 24/7 field services include emergency repairs, modifications, and upgrades of chemical process equipment. Skilled technicians perform high-quality welds and diagnostics on-site, minimizing downtime for clients. This service supports global operations with rapid response teams available for urgent needs.
Graphite Equipment
We supply graphite heat exchangers, columns, and pumps designed for extreme chemical resistance. These products handle corrosive substances like sulfuric acid and hydrochloric acid, leveraging graphite's thermal conductivity and durability. Applications span fertilizer production, metal finishing, and pharmaceuticals.
Pressure Vessels
Custom pressure vessels are crafted to ASME and TEMA standards, tailored for high-pressure and high-temperature environments. Constructed from reactive metals and alloys, they serve in chemical reactors, storage, and processing units, ensuring safety and compliance with global regulations.
HXT Tube Solutions
HXT Tube technology enhances heat exchanger efficiency by 3050% through turbulence-driven fluid dynamics. It prevents sedimentation and fouling in pipelines, optimizing thermal transfer and reducing maintenance costs. This innovation is ideal for chemical transfer and processing systems.
People
Mark Grasso
President & CEO
Mark Grasso leads Apex Engineered Products with over 30 years of experience in industrial engineering. He focuses on strategic growth and innovation, ensuring the company remains a global leader in chemical process equipment.
Sebastian Grasso
General Manager
Sebastian Grasso oversees daily operations, emphasizing quality control and client relations. With 25 years in chemical equipment manufacturing, he ensures efficient project delivery and customer satisfaction.
Adam McGaughey
Sales Manager
Adam McGaughey specializes in chemical process equipment sales, bridging client needs with technical solutions. His expertise in material science supports tailored recommendations for complex industrial applications.
Michael Krzyzewski
Designer & Project Manager
Michael Krzyzewski combines engineering design and project management to deliver precision-crafted equipment. His focus on reactive metals ensures innovative solutions for corrosion-resistant applications.
Mark Evans
Director of Quality
Mark Evans oversees quality assurance, ensuring compliance with ASME, TEMA, and industry-specific standards. His leadership guarantees that all products meet rigorous performance and safety benchmarks.
Questions
What industries does Apex Engineered Products serve?
We serve chemical, petrochemical, chlor-alkali, steel processing, fertilizer, pharmaceutical, and other industries requiring corrosion-resistant equipment.
Do you offer on-site repair services?
Yes, our 24/7 field service team provides on-site repairs, modifications, and upgrades globally for urgent needs.
What materials do you specialize in?
We specialize in titanium, zirconium, tantalum, nickel alloys, and graphite, with expertise in exotic metal fabrication.
Are your products compliant with industry standards?
Yes, our equipment meets ASME, TEMA, and National Board standards, along with certifications from The Chlorine Institute and NACE International.
Can you provide custom solutions?
Yes, we design and fabricate custom heat exchangers, pressure vessels, and process systems tailored to specific client requirements.
Do you offer global shipping and support?
Yes, we serve clients worldwide with manufacturing facilities in the U.S., India, and remote inspection capabilities.
Videos
Reviews (2)
Dominic Tuminello
Jan 03, 2019
Report
I went to this place for an interview. I didn't get hired and I'm not really sure what they build here but the facility was super nice and clean. The staff was extremely polite and helpfull. I'm sure they would be a pleasure to do business with.
George Latkey
May 26, 2018
Report
Very high quality products in production precision with unique Alloys for heat exchangers great employer