Business Details
Engineered Combustion Systems for Industrial Processing
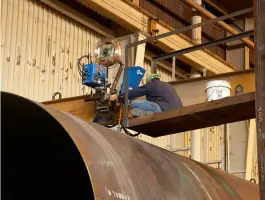
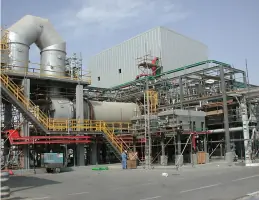
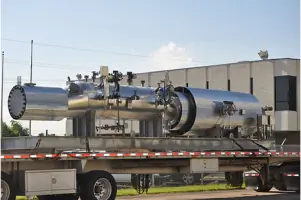
Tulsa Combustion specializes in the design and fabrication of engineered systems for industrial processing applications. Our in-house capabilities span combustion science, thermal treatment, and process engineering, supported by 100,000+ sq ft of manufacturing space. With decades of experience in energy sector projects, our team has developed over 50 patents and pioneered technologies for major energy companies worldwide. We maintain ASME and AWS certifications, employ advanced non-destructive testing protocols, and integrate cross-disciplinary expertise to deliver reliable, code-compliant solutions.Our focus on combustion efficiency, waste treatment, and system integration addresses both large-scale operations and technically unique smaller projects. Through field start-up support and global operational insights, we ensure equipment performance aligns with client safety, environmental, and efficiency objectives.
Services
Midstream Processing
Gasification Systems
Flares
Incinerators
Water Bath Heaters
Direct-Fired Heaters
Burners
Process Skids
Combustion Controls
Highlights and features
- We offer ASME-certified in-house manufacturing for pressure vessels and process systems
- Our staff holds over 50 patents in combustion and thermal treatment technologies
- We provide field start-up support with decades of operational experience
- Our engineers have global project experience across diverse energy markets
- We maintain AWS welding procedures and advanced non-destructive testing protocols
Associations and certifications
- ASME
- AWS
Services
Midstream Processing
We engineer skidded processing units for hydrocarbon treatment including dehydration, amine processing, and cryogenic systems. Our Combined Processing Units integrate multiple functions to reduce footprint while maintaining operational efficiency. These systems incorporate pressure vessels, heat exchangers, and control systems meeting ASME and API standards for midstream petroleum applications.
Flare Systems
Our flare systems safely dispose of waste gases with configurations including ground, enclosed, and offshore designs. We incorporate radiation controls and assist in API 537-compliant installations. The systems feature steam-assisted and air-assisted combustion technologies to meet environmental regulations while ensuring operational reliability in challenging conditions.
Incineration Systems
We design incineration systems for organic waste fluids handling complex combustion challenges. Our solutions include waste heat recovery and effluent treatment components. Systems accommodate variable feed rates while maintaining material durability and personnel safety through engineered quench systems, scrubbers, and advanced combustion controls.
Water Bath Heaters
Our water bath heaters provide controlled heating for multi-phase fluids and viscous hydrocarbons. The systems use submerged coils with precise temperature regulation through heat flux management. Designed for reliability in challenging environments, these heaters incorporate safety features to prevent thermal stress and ensure consistent process fluid heating.
Combustion Controls
We develop burner management systems with safety and flexibility for industrial combustion equipment. Our control panels integrate with plant DCS systems while maintaining Class 1 Div 1 compliance. The systems feature smart controls for NOx reduction, fuel efficiency optimization, and low-emission operation across diverse industrial applications.
Questions
What industrial sectors does Tulsa Combustion serve?
We primarily serve the energy sector with solutions for midstream petroleum processing, waste gas treatment, and thermal system applications across global markets.
Do you provide custom-engineered solutions?
Yes, our in-house engineering team develops tailored combustion and processing systems incorporating proprietary technologies to meet specific project requirements.
What manufacturing certifications do you hold?
We maintain ASME U and S stamps, AWS welding certifications, and implement rigorous non-destructive testing protocols in our 100,000 sq ft facility.
Can you handle international projects?
Our staff has extensive global experience implementing systems in diverse regulatory and environmental conditions across multiple continents.
What after-sales support do you provide?
We offer field start-up assistance, system troubleshooting, and technical support for all installed equipment and retrofits.
How do you ensure system reliability?
Through cross-disciplinary design integration, extensive testing protocols, and leveraging our staff's decades of operational experience in combustion systems.
Reviews (1)
Dwight Tallent
Nov 20, 2021
Report
Tulsa Combustion gave me a guided tour of their facility. I was very impressed to see the effeciency of the assembly and the shipping of their products which go all over the country. Awesome management company. All smiles here.